Sponsored article
Why Does the Same Thicknesser Produce Different Results on Softwood and Hardwood?
- Technical Parameters of the Cutting System
- Feed Speed and Surface Quality
- Effective Chip Extraction as Part of the Process
- How Does Wood Species Affect Planing Performance?
- Wood Moisture Content and Surface Quality
- Grain Direction Matters
- A Stable Machine and Proper Settings Are the Key to Successful Wood Processing
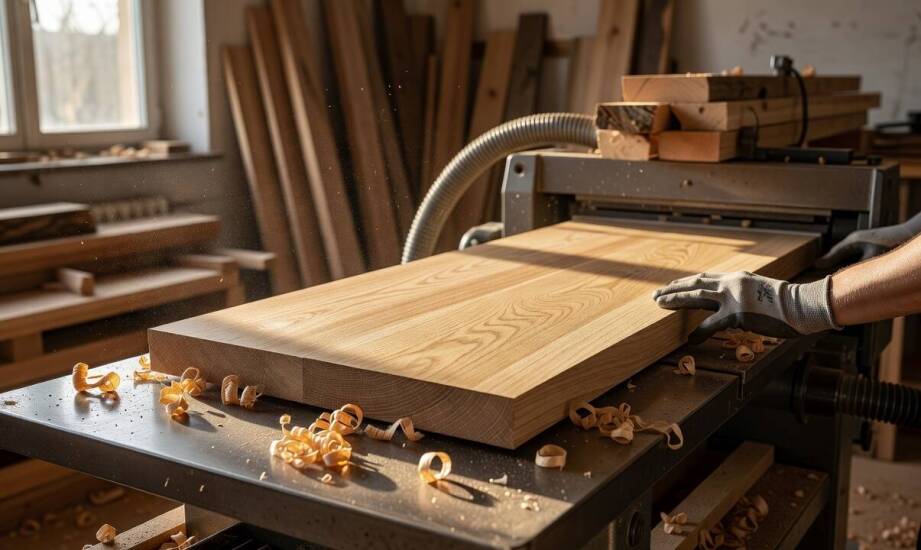
Differences in machining results on softwood and hardwood stem from both the machine's technical parameters and the characteristics of the material itself. Theoretical surface quality assumes operation under ideal, almost laboratory-like conditions. In a real production environment, the final result depends on wood density, moisture content, grain orientation and the precise adjustment of the cutting system. The same machine can create a perfectly smooth surface on a pine board, only to leave noticeable tear-out on an oak plank moments later if the operator fails to adjust the settings accordingly. Understanding cutting mechanics helps avoid costly manual corrections and production downtime.
Read more: What is a priming emulsion and what is its purpose?
Technical Parameters of the Cutting System
The type of cutterhead and the number of knives directly affect the spacing between cut marks on the machined surface. Using a cutterhead equipped with four knives provides a denser cutting pattern, helping to minimise visible waviness on the finished surface.
Read more: How Do Planer Machines, Also Known as Jointers, Work?
Smooth cutter operation also reduces micro-vibrations that can negatively affect the appearance of machined hardwood. Thicknessers supplied by Madora feature robust cast-iron tables and precise lifting mechanisms. These design elements provide stable support and pressure on the workpiece, reducing the risk of lifting or movement during demanding rough machining operations.
Feed Speed and Surface Quality
Serial production requires accurate matching of feed speed to the capabilities of a specific woodworking machine. Thicknesser models available from Madora with a 630 mm working width operate with feed speeds ranging from 4 to 24 m/min, while larger 800 mm and 1000 mm versions work within the 4 to 20 m/min range.
Stepless feed speed adjustment allows a consistent cutting depth to be maintained when machining workpieces with different characteristics. Material is fed evenly through the machine, helping reduce the risk of overloading the main motor when mechanical resistance suddenly increases.
Correct feed speed settings are particularly important when processing hardwood species, which require greater control over the volume of material removed in a single pass.
Effective Chip Extraction as Part of the Process
Proper cutterhead performance also depends on an efficient chip extraction system. An extraction installation with a minimum capacity of 1,750 m³/h and an air velocity of 24 m/s enables continuous removal of chips and dust from the working area.
Efficient extraction helps prevent the build-up of dust and resin on the machine table. As a result, boards can move freely through the machine, supporting consistent machining quality during larger production runs.
How Does Wood Species Affect Planing Performance?
The natural hardness of wood significantly changes the distribution of forces within the cutting chamber during machining. Softwood species generally require relatively low power input during planing, but they often contain a high level of resin.
This sticky substance can accumulate on cutting edges and accelerate tool wear. As a result, material softness alone does not automatically make processing easier.
Hardwood species place much greater mechanical resistance on cutting tools and require more careful feeding through the cutterhead. When machining dense hardwood timber, it may be necessary to reduce the cutting depth per pass. This helps minimise the risk of motor overload and prevents deep imperfections from forming on the wood surface.
Wood Moisture Content and Surface Quality
The hygroscopic condition of the material has a significant influence on the final surface finish. A moisture content of approximately 8% to 12% is commonly considered suitable for many woodworking applications and supports stable machining performance.
When moisture levels are higher, wood fibres may be more prone to deformation during cutting. Excessively wet material can flex under tool pressure, contributing to unevenness and increasing subsequent sanding requirements.
Conversely, heavily overdried wood becomes more brittle, increasing the risk of corner chipping or damage when entering the machining area. Therefore, before starting serial production, it is advisable to check the timber's moisture content and adjust machine settings to the actual condition of the material.
Grain Direction Matters
The orientation of wood fibres has a direct impact on the quality of the finished surface.
Feeding the workpiece in the direction of the grain allows the cutting edges to remove material more cleanly and efficiently.
Cutting against the grain may cause tear-out and cracks extending deeper into the board structure. This issue is particularly visible when machining timber with irregular grain patterns.
Operators can minimise this effect by reducing feed speed and decreasing cutting depth. In practice, even minor adjustments can significantly improve surface quality.
Process automation does not eliminate the importance of operator experience. Variations between individual batches of timber mean that settings effective for one material may not be suitable for another. Evaluating the surface after the first passes provides valuable information on whether feed speed, cutting depth or material handling should be adjusted.
A Stable Machine and Proper Settings Are the Key to Successful Wood Processing
The combination of a stable mechanical system and a thorough understanding of the raw material largely determines process efficiency. A powerful drive system, the correct number of knives and properly calibrated feed rollers enable effective machining of both dense hardwood and resin-rich softwood.
Choosing an industrial thicknesser with appropriate technical parameters can reduce the need for time-consuming recalibration on downstream machines, helping streamline the entire production process.
Conscious management of feed speed, cutting depth and chip extraction performance supports the stable operation of rough machining departments.
Ultimately, it is the combination of the right machine, properly prepared timber and operator expertise that determines production quality and repeatability. A well-organised process allows manufacturers to fully utilise the capabilities of industrial woodworking machinery and transform it into a reliable part of an efficient production line.
You might be interested

Why Invest in a Partnership with a Renowned Vegetable Supplier?
LPG Tanks – Why Invest in the Right Solutions?
The Impact of DAC-7 Regulations on Business Operations in Central and Eastern Europe